Engineers seeking lighter, more formable aluminum sheet for car bodies now have a sharper picture of what happens when a metalworking tool spins through chilled alloy. A new study in Applied Microscopy reports that cryogenic-temperature friction stir processing of AA6xxx aluminum sheet at a relatively low tool rotation speed of 600 RPM produces a finely grained stir zone roughly 1.6 to 1.8 micrometers across at the surface and mid-thickness, while coarser grains of about 4.4 micrometers persist near the bottom of the processed band and in the adjoining thermomechanically affected zone. The work, led by Aman Gupta, Khushahal Thool and Shi-Hoon Choi, combines electron backscatter diffraction, scanning electron microscopy with energy-dispersive spectroscopy, deep-learning-based image segmentation and dense microhardness mapping to link microstructure to mechanical response across the processed region.
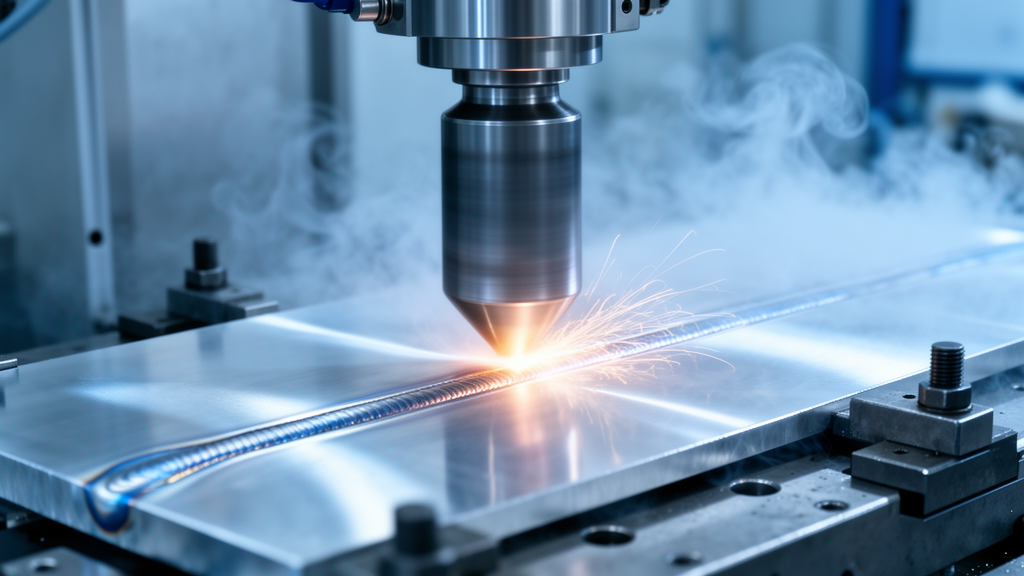
Friction stir processing is a solid-state technique derived from friction stir welding. A rotating, non-consumable tool plunges into the sheet and traverses it, generating intense local plastic deformation and stirring without melting the material. Severe shear and controlled heat input promote subgrain formation, dynamic recovery and dynamic recrystallization, allowing grain sizes to shrink from tens of micrometers to the submicron scale. The method is used to eliminate casting defects, fragment coarse intermetallic phases and create homogeneously refined stir zones that can improve local ductility and formability. Variants of the technique, including multi-pass processing, modified tool geometries and the addition of reinforcing particles, have been explored to tune precipitate fragmentation, particle distribution and grain boundary character.
The twist in the new study is the cooling. In conventional or room-temperature friction stir processing, the thermal cycle can be long enough to allow recovery and precipitate coarsening, which may erode the strengthening contributions of fine precipitates. Cryogenic-temperature friction stir processing instead applies active cooling, typically liquid nitrogen, during tool rotation, sharply reducing the peak and dwell temperatures the material experiences. The lowered thermal budget suppresses recovery and post-deformation grain growth, stabilizes ultrafine grains formed by dynamic recrystallization and raises the fraction of high-angle grain boundaries. It also changes how solutes and second-phase particles behave: reduced temperatures limit extensive dissolution at the solvus but emphasize mechanical fragmentation and rapid, localized reprecipitation, yielding finer and more homogeneous dispersions of magnesium- and iron-bearing precipitates in Al-Mg-Si alloys.
For the experiments, the team used rolled AA6xxx sheet 1.4 millimeters thick, originally strip-cast to 80 percent reduction and solution-annealed at 540 degrees Celsius for 30 minutes. The composition by weight included 1.21 percent silicon, 0.67 percent magnesium, 0.16 percent iron, 0.11 percent manganese and 0.17 percent copper, with minor additions of zinc, chromium, vanadium and titanium. Processing ran along the rolling direction at 600 RPM and 500 millimeters per minute using a heat-treated SKD61 steel tool with a 10 millimeter shoulder and a 3 millimeter pin. Liquid nitrogen, delivered continuously from a rear-mounted nozzle at an approximate working temperature of minus 50 degrees Celsius, provided in-process cooling. The resulting processed band was about 10 millimeters wide, and local sheet thickness within the stirred region was reduced to roughly 1.2 millimeters.
Orientation microscopy revealed a strongly heterogeneous but largely refined microstructure. At the surface, where the rotating shoulder imposes high strain rates, the average grain size was 1.7 plus or minus 0.7 micrometers with a kernel average misorientation of 1.9 degrees, consistent with extensive dynamic recrystallization and reduced dislocation density. The center of the stir zone remained equiaxed and uniformly refined at about 1.75 micrometers with a slightly lower misorientation of roughly 1.7 degrees, indicating a balanced temperature-strain environment at the core. Near the bottom, at the interface between the stir zone and the thermomechanically affected zone, grains coarsened to about 4.4 plus or minus 5.4 micrometers with a misorientation near 1.94 degrees, and fine recrystallized grains appeared along the boundaries of coarser grains bearing strong orientation gradients, the signature of a partially recovered thermomechanically affected zone.
Grain boundary statistics reinforced this picture. The center of the stir zone showed a high-angle grain boundary fraction of about 79 percent with a low-angle fraction near 18 percent, and the surface showed about 75 percent high-angle boundaries, both confirming substantial recrystallization. At the advancing side the high-angle fraction dropped to roughly 64 percent as low-angle boundaries rose to about 31 percent, and at the bottom it fell further to about 56 percent with 36 percent low-angle boundaries, reflecting incomplete recrystallization where strain and cooling are weaker. The retreating side, with elongated and distorted grains averaging 10.5 plus or minus 7 micrometers and low misorientation values up to 1.6 degrees, showed the least deformation. Recrystallized grain fractions quantified with a grain orientation spread threshold of 1.5 degrees or less reached 67 to 71 percent at the center and surface but fell to 58 percent at the advancing side, 45 percent at the bottom and just 12 percent at the retreating side. Coincidence site lattice boundaries of the sigma-3 and sigma-9 types were slightly more prevalent in the stir zone, at 3 to 4 percent, than in the thermomechanically affected zone, below 2 percent.
The second-phase particles told a parallel story. In the as-received sheet, dark near-spherical particles corresponded to Mg2Si and grey elongated particles to Al-Fe-Si intermetallics, distributed heterogeneously along the rolling direction and often segregated at grain boundaries. Image-based quantification put the average Al-Fe-Si particle size near 4 micrometers, with Mg2Si particles ranging from 0.8 to 1 micrometer. Deep-learning segmentation of scanning electron micrographs, built on a U-Net architecture trained with a hybrid Dice and categorical focal loss, then quantified how these populations evolved. Mean equivalent-circle diameters fell from 0.97 plus or minus 0.63 micrometers for Al-Fe-Si and 0.80 plus or minus 0.47 micrometers for Mg2Si in the as-received sheet to about 0.63 plus or minus 0.40 micrometers for Al-Fe-Si at the surface and 0.65 plus or minus 0.35 micrometers for Mg2Si at the bottom, with reduced nearest-neighbor spacing in the stir zone. The surface and center held finer, more uniformly dispersed particles, while the bottom retained larger, sparser coarse particles.
Not every trend moved in the same direction. Nearest-neighbor spacing for Al-Fe-Si decreased at the surface, center and bottom, with the smallest spacing of about 3.73 plus or minus 2.63 micrometers at the bottom, but Mg2Si nearest-neighbor distances generally increased in the processed regions relative to the starting material, reaching 8.02 to 11.38 micrometers where recrystallization was strong. The authors interpret this as substantial dissolution of Mg2Si during processing with limited reprecipitation under rapid cryogenic cooling. Energy-dispersive analysis supported the particle identifications: Mg2Si regions showed elevated magnesium and silicon, Al-Fe-Si particles were enriched in iron and silicon with minor magnesium, cobalt and manganese, and one coarse grey particle with roughly 26 percent silicon suggested a relatively uncommon Al-Si intermetallic. After processing, measured magnesium near 1.01 percent and silicon near 0.77 percent appeared more uniformly distributed in the matrix.
Hardness mapped the consequences. The as-received sheet measured 87 plus or minus 6 Hv. In the processed sample, the stir zone softened to between 64 and 73 Hv, the thermomechanically affected zone hardened moderately to 77 to 83 Hv, and regions farther from the stir zone boundary reached 86 to 93 Hv. The softening arises because precipitate dissolution and dynamic softening reduce dislocation density, and the loss of precipitate and solute strengthening outweighs the Hall-Petch gains expected from finer grains. Hardening outside the stir zone instead reflects numerous subgrains with high dislocation density and retained or reprecipitated particles, with grain boundary pinning and geometrically necessary dislocations from strain incompatibility contributing. The authors identify continuous dynamic recrystallization, assisted by dynamic recovery, as the dominant softening mechanism, consistent with prior electron microscopy studies on friction stir processed aluminum alloys.
Compared with the team’s earlier work at 800 RPM, the lower 600 RPM speed produced a more heterogeneous grain size distribution and slightly higher misorientation values, likely from increased strain accumulation at reduced heat input, and a more pronounced through-thickness contrast in particle size and spacing. The authors note that regional selection can influence quantitative values and that both tool rotation speed and cooling strategy shape the final microstructure. They frame the quantitative particle metrics and hardness gradients as guidance for choosing cryogenic friction stir processing parameters that balance grain refinement against precipitation strengthening in automotive sheet applications, where improved bendability and delayed crack initiation have been linked to homogeneous recrystallization and reduced strain localization under cryogenic cooling.
Subject of Research: Microstructure, second-phase particle evolution and hardness in cryogenic-temperature friction stir processed AA6xxx aluminum sheet
Article Title: Orientation microscopy study of cryogenic-temperature friction stir processed AA6xxx sheet: microstructure and second phase particles evolution
Article References: Gupta, A., Thool, K., & Choi, S.-H. (2026). Orientation microscopy study of cryogenic-temperature friction stir processed AA6xxx sheet: microstructure and second phase particles evolution. Applied Microscopy, 56(1), Article 20. https://doi.org/10.1186/s42649-026-00133-x
Image Credits: AI Generated
DOI: 10.1186/s42649-026-00133-x
Keywords: friction stir processing, AA6xxx aluminum alloy, cryogenic cooling, liquid nitrogen, electron backscatter diffraction, dynamic recrystallization, Mg2Si precipitates, Al-Fe-Si intermetallics, deep learning segmentation, microhardness, grain refinement, automotive sheet
News Source: Neil Sanderson. (October 28, 2026). Cryogenic friction stir processing refines AA6xxx aluminum sheet grains and particles. Scienmag.