Hot mix asphalt is one of those materials the public rarely thinks about until a road begins to fail, yet its production is a finely balanced industrial process. A typical mixture contains roughly 5 percent bituminous binder and 95 percent mineral aggregates such as crushed stone, gravel, sand, filler, or reclaimed asphalt pavement, heated to between 140 and 170 degrees Celsius so the binder coats the aggregate properly. Now, researchers analyzing three years of internal quality control data from a single batch-type asphalt mixing plant in Lithuania have shown that the deviations of the mixture’s actual components from their design targets can be treated statistically, allowing the plant’s production capability to be scored with two widely used manufacturing indices.
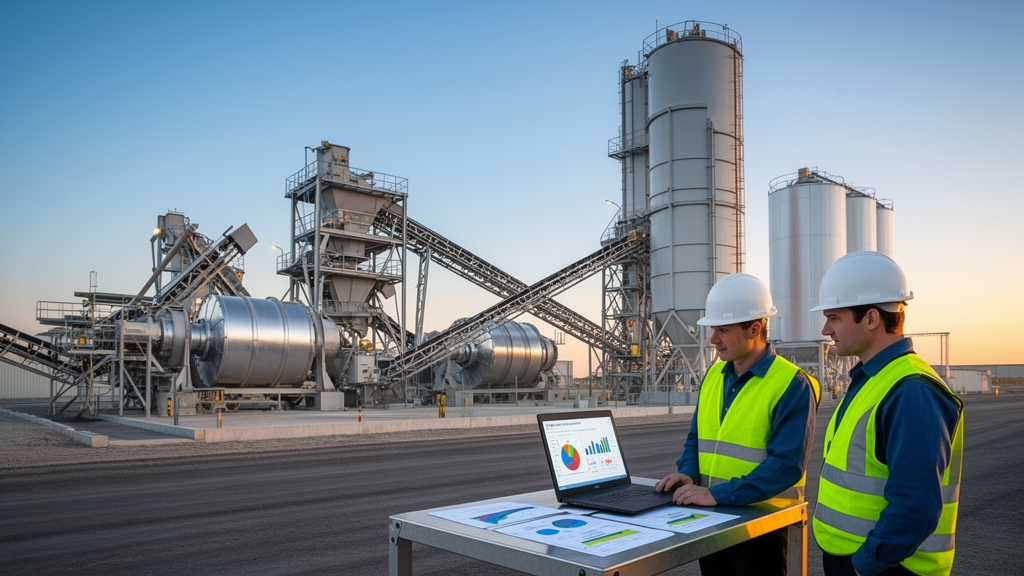
The study, published in Case Studies in Construction Materials, focused on a Benninghoven TBA 4000 UC batch plant with a rated capacity of 320 tonnes per hour and a 4000-kilogram batch mass. The team examined asphalt concrete mixtures with nominal maximum particle sizes of 11, 16 and 22 millimetres, drawing one or two representative quality control samples on production days. In total, 533 samples were analyzed: 102 in 2018, 146 in 2019 and 285 in 2020, each extracted to separate the bitumen from the mineral fraction before sieving determined the gradation of the aggregate.
Every sample was compared against the job mix formula, the design recipe that specifies the target percentage of each constituent. The researchers calculated deviations for six controlled components: bitumen binder content, mineral filler passing the 0.063 millimetre sieve, particles passing the 0.125 millimetre sieve, fine aggregate between 0.063 and 2 millimetres, coarse aggregate larger than 2 millimetres, and particles exceeding the maximum aggregate size. A key mathematical insight underpinned the whole approach: subtracting a constant design value from every measurement does not change the variance, so the standard deviation of the deviations from the job mix formula is identical to the standard deviation of the absolute contents. This meant mixtures of different designs produced across an entire season could be pooled into a single statistical population.
The deviations proved to follow a normal distribution, confirmed by skewness and kurtosis values that stayed below their critical thresholds for every component and every year. For bitumen binder, the mean deviations hovered near zero at 0.07 percent in 2018, 0.001 percent in 2019 and 0.03 percent in 2020, while the standard deviations fell steadily from 0.25 to 0.23 to 0.20 percent. That downward trend in variability signals improving production consistency, a change the authors attribute partly to a regulatory tightening in mid-2018, when the allowable binder deviation dropped from plus or minus 0.5 percent to plus or minus 0.3 percent of the mixture mass.
Defect rates told a similar story. The share of samples failing the binder tolerance fell from 19.6 percent in 2018 to 6.8 percent in 2019 and 4.9 percent in 2020, with the elevated 2018 figure reflecting the stricter limit applied retroactively to that season’s data. Mineral filler content produced no non-compliant results at all, defects in the fraction below 0.125 millimetres fell from 1.0 percent to zero, fine aggregate defects declined from 5.9 to 3.5 percent, and oversize particle defects dropped from 2.0 to 1.1 percent. Binder content was consistently the dominant source of non-conformity, underscoring how demanding the tightest tolerance in the specification is for plant dosing systems.
Mixture type mattered as well. The binder content standard deviation was lowest for the fine-graded AC 11 mixture and highest for the coarse AC 22, and across all three types it declined over the study period. The finest fractions showed their largest variation in AC 11, influenced by dosing errors of imported filler and reclaimed dust, whereas the AC 22 mixture, containing the least of these fine particles, varied minimally and grew slightly more homogeneous. Conversely, the fine aggregate, coarse aggregate and maximum-size fractions varied most in AC 22, which the authors link to segregation processes that disproportionately affect coarser mixtures.
With the location and dispersion parameters established, the team computed the process capability indices Cp and Cpk, borrowed from manufacturing and service industries, where they quantify whether a process can reliably hold output within specification limits. Cp measures dispersion alone, while Cpk also captures how well the process is centered between the lower and upper specification limits. The lowest index values appeared for bitumen binder content and the highest for mineral filler and the 0.125 millimetre fraction, and both indices showed an improving trend across the three years, approaching recommended minimum levels from the quality engineering literature.
The comparison with earlier work proved instructive. Divinsky and colleagues had previously evaluated six asphalt mixing plants, reporting a mean binder standard deviation of 0.15 percent against 0.23 percent in the Lithuanian study, with correspondingly higher capability indices for binder but lower ones for mineral filler. The authors note these results are close enough to suggest that over the last fifteen to twenty years the capacity of modern plants to meet component tolerances has been sufficient and relatively stable, though tightening tolerances further would inevitably raise defect counts. A centering coefficient K, calculated from the ratio of the two indices, averaged between zero for binder and 0.22 for fine aggregate and also declined over time.
Perhaps the most practical outcome is the regression linking capability to defects. Quadratic models showed that as the percentage of non-compliant samples rises, Cp and Cpk fall, with coefficients of determination of 0.757 and 0.800 respectively. Setting the defect rate to zero implies Cp must reach at least 1.45 and Cpk at least 1.23, while an engineering-acceptable 5 percent defect rate corresponds to Cp of 0.72 and Cpk of 0.62. These thresholds align with values recommended in statistical process control, giving plant operators concrete numerical targets.
The authors caution that the indices can only be computed for constituents with defined specification limits, and that older or technologically outdated installations may struggle to satisfy progressively stricter tolerances even as automated control systems improve. They recommend evaluating plant capability annually after each construction season using a sufficiently large and representative quality control dataset. For an industry running roughly 4000 plants in Europe and 4500 in the United States, where quality control already consumes about 2 percent of construction costs and poor quality can trigger far costlier repaving, the message is that long-established paving materials still yield to modern statistical scrutiny.
Subject of Research: Statistical process capability assessment of hot mix asphalt production based on component deviations from the job mix formula
Article Title: Determination of process capability indices for a batch asphalt mixing plant based on hot-mix asphalt component deviations from the job mix formula and allowable tolerance
Article References: Sivilevičius, H., Mickevič, R., Škulteckė, J., Šernas, O., & Vaitkus, A. (2026). Determination of process capability indices for a batch asphalt mixing plant based on hot-mix asphalt component deviations from the job mix formula and allowable tolerance. Case Studies in Construction Materials, 25, Article e06645. https://doi.org/10.1016/j.cscm.2026.e06645
Image Credits: AI Generated
DOI: 10.1016/j.cscm.2026.e06645
Keywords: hot mix asphalt, asphalt mixing plant, process capability indices, job mix formula, quality control, bitumen binder content, aggregate gradation, statistical process control, batch plant, pavement engineering, construction materials, Determination
News Source: Denise Maddox. (October 23, 2026). Statistical Indices Score Asphalt Plant Quality From Three Years of Production Data. Scienmag.